If you’ve ever sat in a production meeting for custom metal parts, you’ve probably heard the term “blanking line” tossed around without a full breakdown of what it means—especially if you’re new to the manufacturing supply chain. But if you’re a spreadsheet user, that same term has a whole other, equally critical meaning when it comes to how you model, cost, and optimize blanking line operations. As a supplier of industrial blanking lines, I spend half my time on the factory floor troubleshooting equipment, and the other half walking clients through spreadsheets that keep their production on track. That dual perspective makes the gap between spreadsheets and physical manufacturing feel a lot smaller than most people assume. Let’s break down how “blanking lines” work in a spreadsheet formula, how that translates to the machines we build, and why getting both right saves you time and money. Blanking Lines
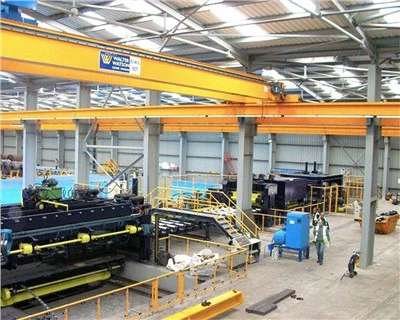
First, let’s get clear on terminology. A blanking line, in the manufacturing sense, is a production setup that cuts large metal coils into smaller, standardized pieces (called blanks) for parts like car body panels, appliance housings, or industrial brackets. But in a spreadsheet formula, a blanking line is a set of logical rules that automate how you calculate everything from material usage to equipment run time to labor costs for those blanks. A lot of manufacturing teams treat these two separate: they design their process on a machine, then plug numbers into a spreadsheet. The smart ones? They build the spreadsheet formula to mirror the physical blanking line’s constraints. That’s where the magic happens.
Let’s start with the basics of a spreadsheet formula. Most spreadsheets use simple arithmetic, but formulas get powerful when you add conditional logic—IF statements, COUNTIF, SUMIF, or INDEX/MATCH. A blanking line formula isn’t just a number; it’s a chain of rules that account for the limits of both your spreadsheet and your physical equipment. For example, if you’re cutting blanks from a 12-foot steel coil, your physical blanking line can’t cut a blank longer than 10 feet (that’s the maximum tool stroke on most entry-level lines). A basic spreadsheet formula for total blanks per coil would look like something you’d learn in a beginner course: =INT((Coil Length - Waste Trim) / Blank Length). That’s simple, right? But that formula fails every time the physical line has another constraint—like a minimum trim length, or a required gap between blanks to prevent edge burrs. That’s where the “blanking line” logic stops being basic math and starts being tailored to your equipment.
Here’s a real example from a client I worked with last quarter. They made custom HVAC brackets, and their initial spreadsheet formula was missing key physical constraints of their new blanking line. The formula they used was = (Total Order Length) / (Blank Length), and it left them ordering 15% more steel than they needed. Why? Their blanking line’s shear required a 2-inch gap between every blank, plus a 6-inch trim piece at the start and end of each coil. The client’s formula didn’t account for those, so when they cut a 10-foot coil, they’d try to fit four 2.3-foot blanks, but the gap and trim left only 9 feet usable—so they only got three blanks per coil instead of four. That small miscalculation added up to thousands of dollars in extra material costs per month. Once they adjusted their formula to mirror their line’s physical rules, that waste vanished.
So what does a functional blanking line formula look like? Let’s build it step by step, using real values from that HVAC bracket client. First, define the fixed constraints of your physical blanking line—these are non-negotiables. For this example, let’s call them:
Coil Length = 120 inches(standard steel coil width for HVAC parts)Min Trim Length = 6 inches(required to protect the shear tool)Gap Between Blanks = 2 inches(prevents burrs on cut edges)Blank Width = 27 inches(the width of each HVAC bracket blank)
Next, add conditional logic for how many blanks fit per coil. The usable length of the coil is total length minus two trim pieces (one at the start, one at the end): Usable Length = Coil Length - 2 * Min Trim Length. Then, the total length one blank plus its required gap takes up is Blank + Gap = Blank Width + Gap Between Blanks. But wait—the last blank in the coil doesn’t need a gap after it, right? That’s a common mistake in beginner formulas. If you divide usable length by (Blank + Gap) and round down, you end up with one blank too few, because the final gap isn’t required. So adjust that to: Number of Blanks per Coil = INT( (Usable Length) / (Blank + Gap) ) + 1. Let’s test that math with our numbers: Usable Length = 120 - 12 = 108 inches. Blank + Gap = 27 + 2 = 29 inches. 108 divided by 29 is ~3.72, so INT gives 3, plus 1 is 4 blanks. Perfect—exactly what we wanted, no waste.
But the formula doesn’t stop at count. A good spreadsheet blanking line also calculates labor time, equipment run time, and material cost. For example, if your blanking line runs 10 feet per minute, and it takes 2 minutes to load a coil, the total time per coil is = (Number of Coils) * (Load Time + (Usable Length / Run Speed)). That’s not just math—it’s a direct reflection of how the machine works. A lot of teams use generic time tracking formulas, but when you tie the time calculation to your specific blanking line’s speed, you get way more accurate scheduling. I’ve seen clients cut their lead times by 10% just by fixing their formula to match their equipment’s actual run rate, instead of a generic industry average.
Now, let’s talk about the edge cases that trip up even experienced users. Blanking lines aren’t just perfect—they have downtime, scrap rates, and coil variations. A solid formula will account for that. For example, if your line has a 2% scrap rate (meaning 2 out of every 100 blanks get ruined in a cut), your formula needs to add a buffer: Total Blanks Needed = Order Quantity / (1 - Scrap Rate). If your client needs 1,000 good blanks, 1,000 divided by 0.98 is ~1,020 total blanks to order. That’s a small buffer, but it keeps you from missing a production run because a small number of blanks got scraped. Another edge case: if a blank is too short for your line’s minimum size. If your physical line won’t cut a blank smaller than 10 inches, your formula should flag any blank under that size as invalid, so you don’t waste time trying to cut something the machine can’t handle.
Here’s where my role as a blanking line supplier ties this all together. When I install a new blanking line at a factory, I don’t just hand over the machine keys and a user manual. I spend a full day working with their operations team to audit their existing spreadsheets, because most of them have hidden gaps between their formulas and their equipment. For example, a mid-sized auto parts plant in Ohio I worked with last year had a spreadsheet that assumed their line ran 20 feet per minute, but the actual line had a variable speed: it runs faster for wide blanks and slower for narrow ones. Their formula was overestimating production speed, leading them to understaff shifts and miss deadlines. We rewrote their formula to pull real-time speed data from the line’s control system (something as simple as a VLOOKUP that matches blank width to run speed) and cut their missed deadlines by 80% in three months.
Another common mistake: people use static numbers in their formulas, instead of linking them to the line’s controls. If you change the blank size you’re cutting, you don’t want to have to manually update 10 different cells in your spreadsheet. Instead, make your formula pull the blank width from a single cell that you update when you change the die on your blanking line. That way, if you switch from a 10-inch bracket to a 15-inch bracket, you just edit one cell, and all your calculations for blanks per coil, run time, and cost update automatically. It’s a small tweak, but it eliminates human error and saves hours of work every week.
Now, let’s address why this matters for anyone in manufacturing, not just spreadsheet nerds. A blanking line is a big investment—most of the lines we build start at $50,000 and go up to millions for high-volume operations. If your spreadsheet formula doesn’t align with how that line works, you’re leaving money on the table. We’ve had clients who upgraded their blanking line and didn’t adjust their formulas, so they still used the old line’s constraints. That meant they were using 20% more material and running the line 15% slower than they could. Fixing the formulas was a free fix, but they didn’t realize it until we walked them through the numbers.
I also want to clear up a common myth: you don’t need an advanced degree in data science to build a good spreadsheet blanking line. Most of the formulas I see clients use are combinations of basic functions: INT, IF, VLOOKUP, and simple arithmetic. The key is not the complexity of the formula, but the accuracy of the rules you build into it—rules that match your physical line’s limits, your material waste, and your production needs. You don’t need to run a simulation or use a fancy add-on; you just need to ask: “What does my blanking line actually do, and how do I translate that into a number?”
For anyone who’s building or updating their spreadsheet formulas, here’s a quick checklist I give every new client:
- List every non-negotiable constraint of your blanking line: maximum blank size, minimum trim, gaps between blanks, run speed, scrap rate. Write these down before you open your spreadsheet.
- Avoid hardcoding numbers into formulas. Link each constraint to a separate input cell, so you can update it if you change dies, get new coils, or adjust line speed.
- Test your formula with real, small-scale runs. Cut a single coil, count how many blanks you get, and compare it to your formula’s output. If it’s off by more than 1, you missed a constraint.
- Add error checking. Use IFERROR functions to flag if a blank size is too small, a coil is too short, or you don’t have enough material to fill an order. That way, you don’t find out about a problem mid-production.
At the end of the day, the line between the spreadsheet “blanking line” and the physical machine in your shop is a lot thinner than you might think. I’ve spent enough time on both sides to know that the best manufacturing operations are the ones that don’t treat spreadsheets and equipment as separate. When your formula works with your line, not against it, you get less waste, faster lead times, and a team that doesn’t have to play catch-up with bad numbers.

If you’re currently looking to upgrade your blanking line, optimize your current setup, or just want to walk through your spreadsheet formulas to make sure they’re aligned with your production needs, let’s connect. We work with shops of all sizes, from small job shops to large OEMs, to make sure their equipment and their spreadsheets work in sync. There’s no one-size-fits-all solution, but we can help you find the right setup for your production goals.
Cut To Length Line References
- Kalpakjian, S., & Schmid, S. R. (2014). Manufacturing Processes for Engineering Materials (6th ed.). Pearson.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). Wiley.
- National Metalforming Association. (2022). Best Practices for Blanking Line Operations and Cost Estimation.
- Microsoft Support. (2023). Guide to Building Conditional Formulas in Excel for Manufacturing Use Cases.
Shanghai HOYO Industries Co., Ltd.
Shanghai HOYO Industries Co., Ltd. is one of the most professional blanking lines manufacturers and suppliers in China, featured by quality products and competitive price. Please rest assured to buy cheap blanking lines for sale here from our factory. Contact us for customized service.
Address: No.8, Jianding Road, Fengjing Town, Jinshan District, Shanghai, China
E-mail: info@hoyomachinery.com
WebSite: https://www.hoyomachinery.com/
